 Technology News
News
Stay updated with JJY Laser's latest news, breakthroughs, and industry insights
Technology News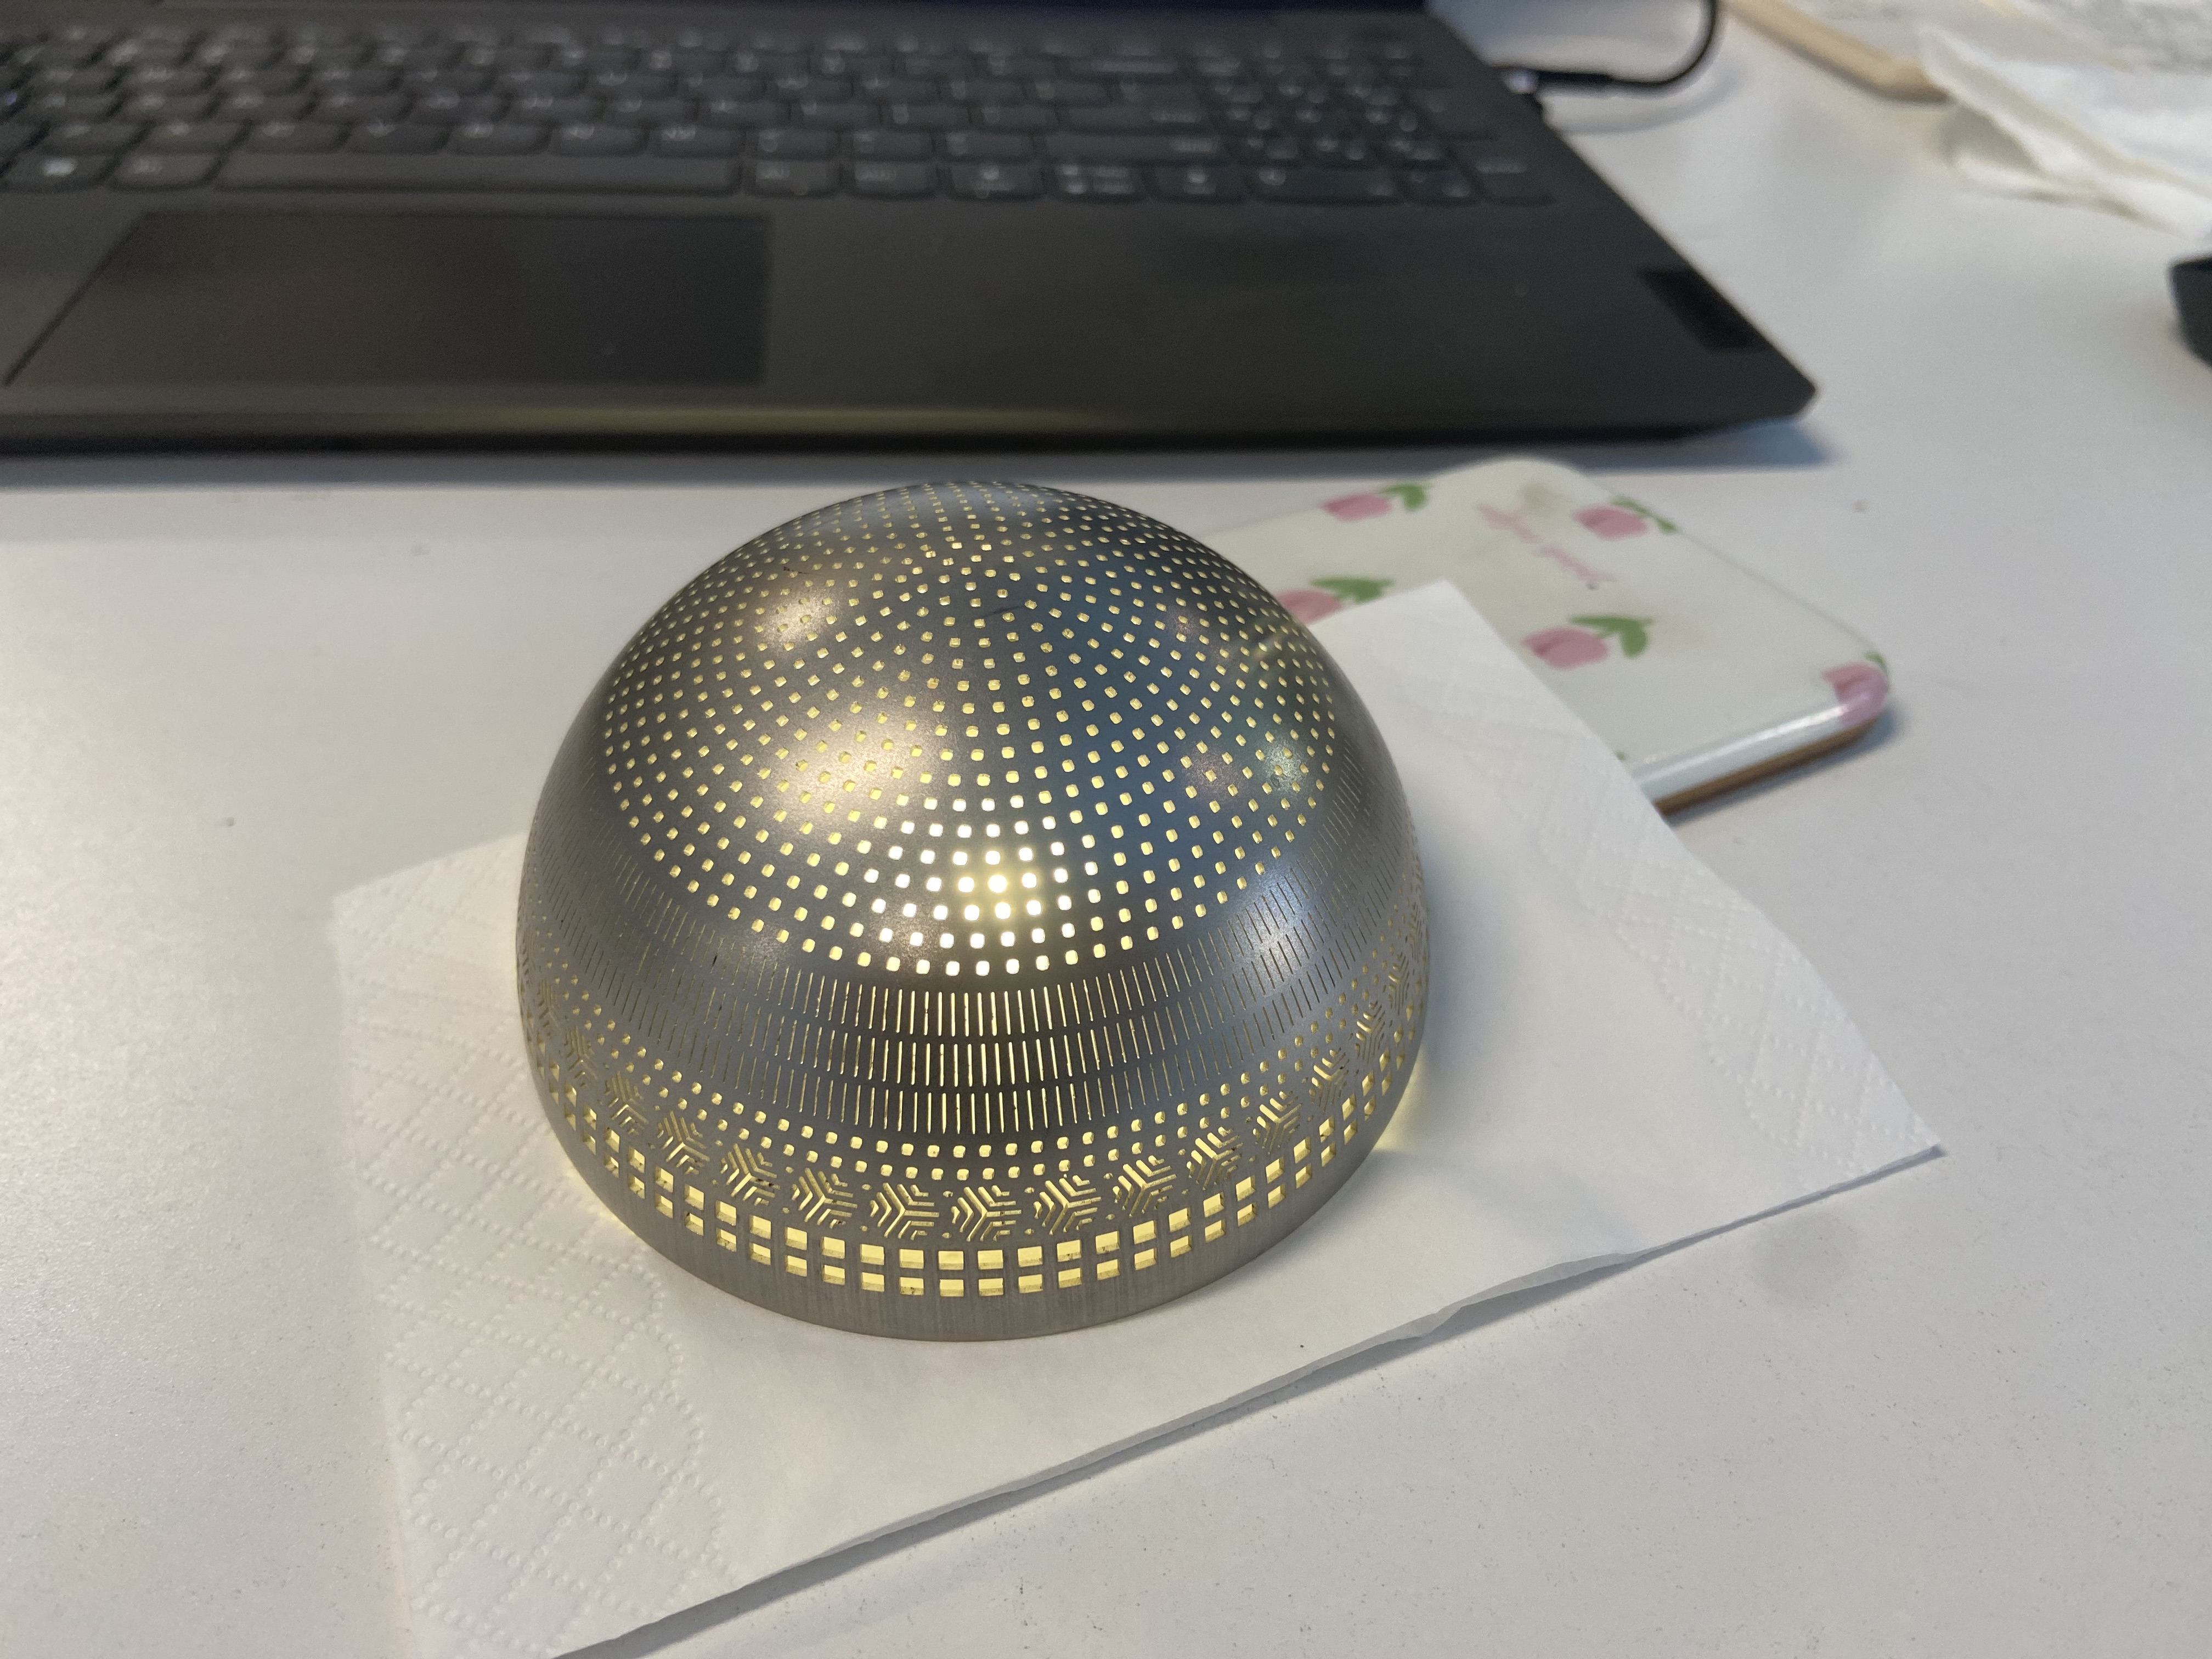 Technology News
Drilling 1600 special-shaped micro-holes on a hemispherical surface: Why traditional processes are incapable of realizing this requirement, and how Jiajiayong 5-axis laser processing breaks this technical bottleneck?
A few days ago, the owner of a manufacturer specialized in precision filtration and atomization components came to me with a set of engineering drawings. He raised a processing requirement to machine 1,600 holes on a hemispherical surface that is 10cm in outer diameter and 1mm in wall thickness: 1,000 round holes with a 0.1mm aperture, 300 square holes with a side length of 0.5mm, 200 elongated slotted holes measuring 1cm × 0.2mm, and 100 special-shaped profiled holes. All holes are designed with a 0.3mm adjacent hole pitch, and zero burrs is set as a non-negotiable acceptance standard.
View Details Technology News
Over 10 million holes with a diameter of 0.1 mm: how can this drilling task be realized with conventional mechanical machining drilling processes?
Fellow practitioners in the sectors that manufacture filter screens, spinneret plates, atomizing discs and flow control plates have almost all come across this type of order: the customer requires tens of millions of micro-holes to be drilled on a single plate, with a pore diameter of 0.1mm, and the finished part must meet the requirements of zero burr, no deformation, and 100% pore penetration rate.
View Details Technology News
Key Quality Control Points for Laser Drilling of Mold Venting System: The Underlying Engineering Logic Behind the Surface Roughness Requirement of Ra < 0.4 μm
All practitioners in the mold manufacturing industry well know that the quality of vent holes is never qualified enough by the lazy, oversimplified standard of "getting the hole drilled through is all it takes". Every indicator including hole wall roughness, edge burrs, microcracks and recast layer thickness directly affects the venting efficiency and service life of the vents.
View Details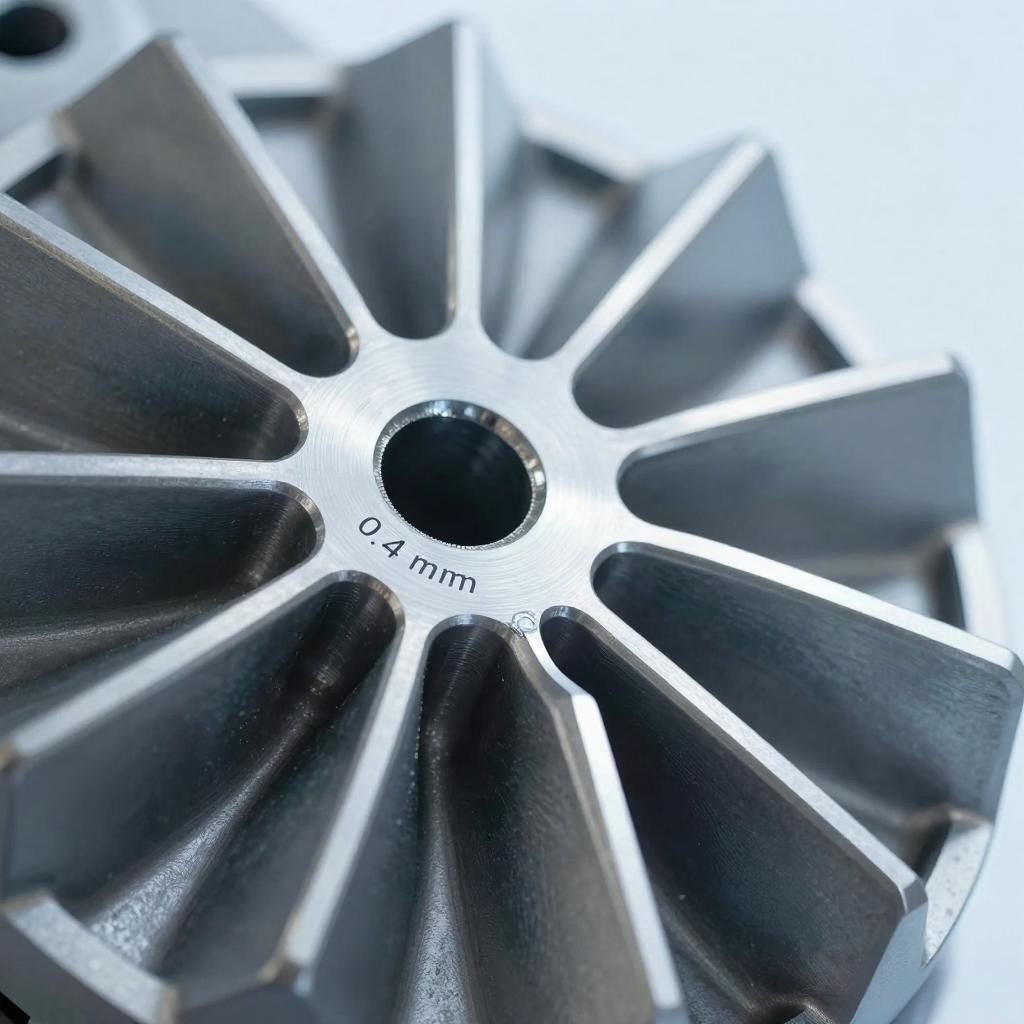 Solutions News
Aerospace High-Precision Oil Filter Screen Micro-Hole Laser Forming Solution — Jiajia Laser One-Step Forming Technology for Main Hole + High-Pressure Auxiliary Hole
In the fuel and lubricating oil systems of aero-engines, the oil filter screen acts as the "last line of defense" to guarantee the safe operation of the engine. Once fine particles in the fuel enter the combustion chamber, they may cause fuel nozzle clogging, combustion efficiency degradation, and even in-flight engine shutdown. Contaminants in the lube oil system, on the other hand, will lead to bearing abrasion and rotor scoring, directly threatening the engine's service life and flight safety.
View DetailsTechnology NewsLaser Drilling Technology for Cooling Holes on Special-shaped Ejector Plates: One-time Integral Forming of Complex Curved Surfaces, Inclined Holes and Circumferential Holes
All peers engaged in injection mold and die-casting mold manufacturing are well aware that the cooling performance of the ejector plate directly determines the molding cycle and finished part quality. This is especially true for special-shaped ejector plates, which are embedded with cooling holes distributed on curved surfaces, inclined planes and in circumferential arrays. Conventional mechanical drilling technology can barely cope with such processing demands: the drill bit fails to achieve normal perpendicular positioning on curved surfaces, complex custom jigs and fixtures are required for inclined hole machining, and the pitch consistency of circumferential hole arrays is far from guaranteed.
View Details Industry News
Selection Guide for Fully Automatic Laser Drilling Equipment for Stainless Steel Flow Orifice Machining
Anyone working in the hardware processing, fluid control component and filtration equipment industries knows full well that machining stainless steel flow orifices is far from the trivial task of simply "drilling a random hole". A mere 0.1mm aperture deviation, when amplified by hydrodynamic (fluid mechanics) effects, can easily drive the flow rate error far beyond the customer's specified acceptance tolerance range.
View Details Technology News
Laser Drilling for Gas Stove Burner Nozzles: The Process Logic Spanning From Aperture Precision to Combustion Efficiency
Anyone engaged in the gas appliance industry is fully aware that the aperture precision of gas burner nozzles directly dictates combustion efficiency. An over-sized aperture will cause excess gas supply, red-colored flame, and carbon monoxide (CO) emissions exceeding regulatory safety limits. An undersized aperture leads to insufficient heat output and ignition difficulty. If burrs exist on the inner wall of the nozzle orifice, the airflow will turn turbulent, resulting in unstable flame operation.
View Details Technology News
Analysis of Femtosecond Laser Micro-hole Machining Process for H13 Tool Steel: How to Achieve No Microcracks under Scanning Electron Microscopy (SEM)
H13 is no stranger to peers engaged in mold manufacturing: it is one of the most commonly used hot work tool steels, featuring high hardness, good toughness and excellent thermal fatigue resistance. However, it is precisely because of these "advantages" that it has also become one of the most difficult-to-machine tool steels.
View Details Company News
Integrated Laser Equipment Solution for Cutting and Punching Electronic Products: One machine for multiple uses, efficiency doubled.
In electronic product manufacturing, cutting and punching are typically two consecutive processes.For example, for flexible printed circuits (FPC), the outer shape needs to be cut first, followed by punching positioning holes and vias; for sensor housings, after cutting the product contour, mounting holes and ventilation holes are drilled; even for some metal shielding covers, both edge trimming and heat dissipation hole punching are required.
View DetailsPer pageitems|Total 48 items